
Heat Aging Testing for Elastomers: Oven Effects on Hardness, Tensile, and Elongation
What ASTM D573 / ISO 188 heat aging means for O-Rings: air-oven method, hardness rise and tensile/elongation retention, D2000 screen temperatures, family heat rankings, and how seal engineers read the datasheet beside compression set and TR-10.
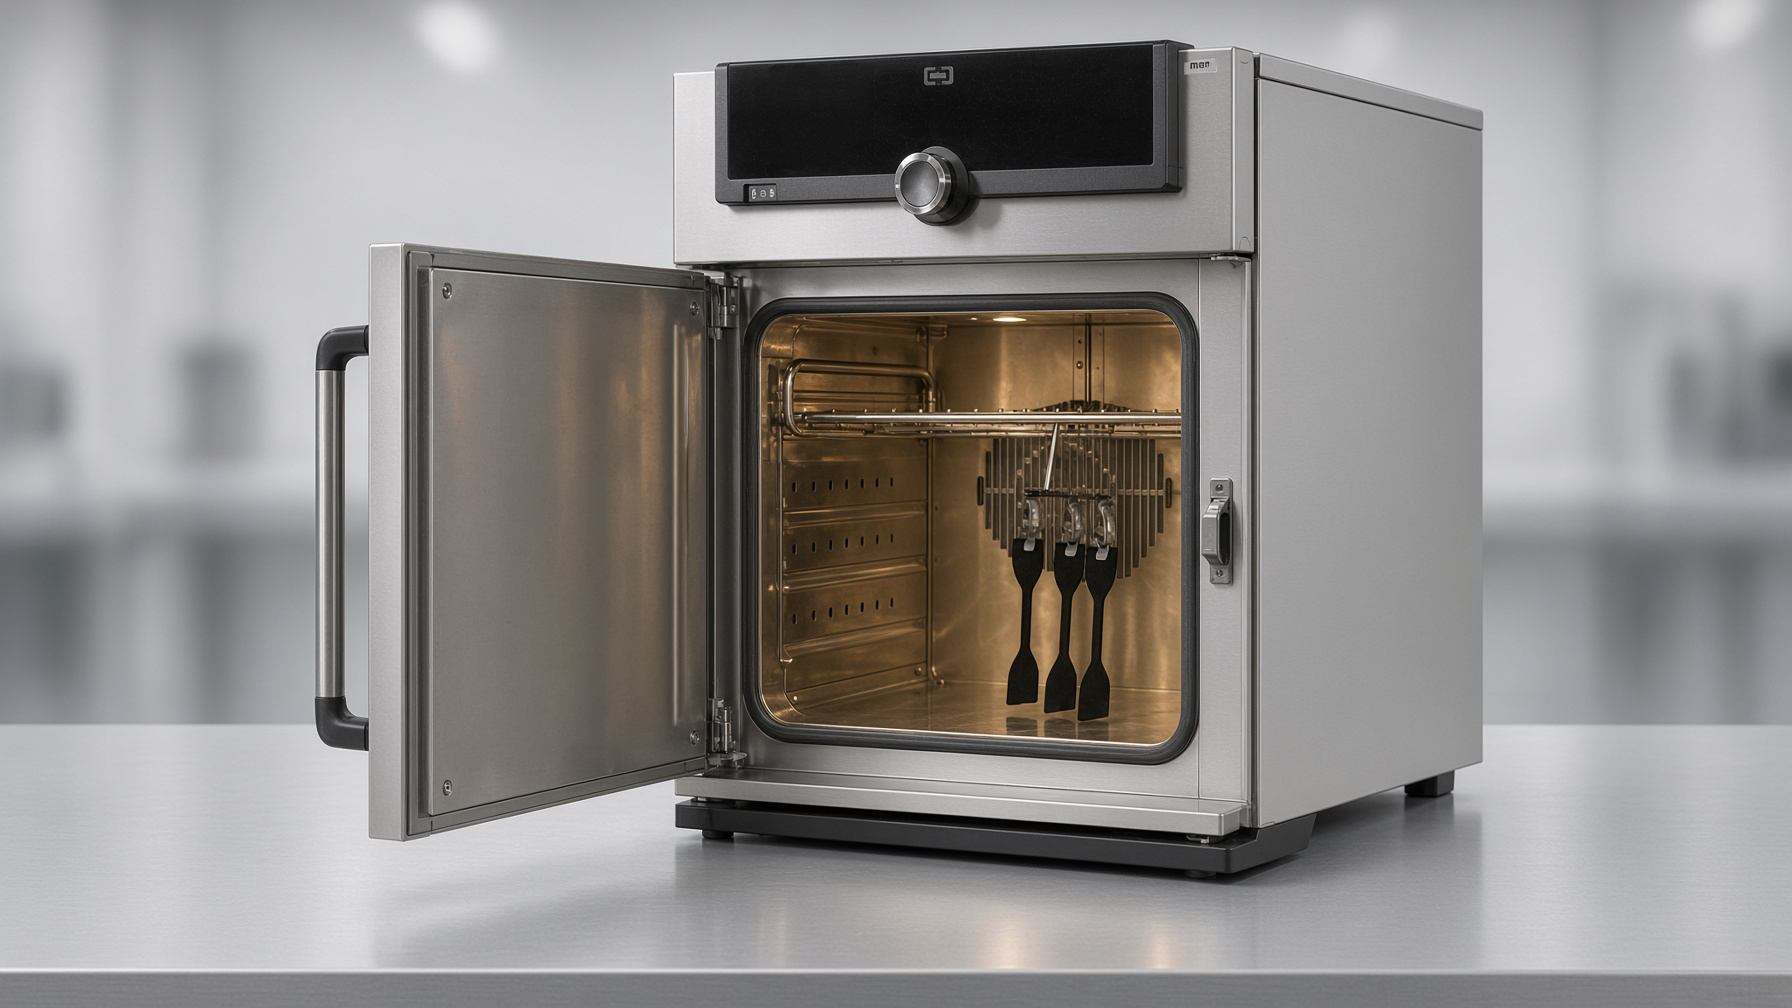
Heat aging is the dry-oven number that predicts whether an O-Ring will stay tough after living in hot air. ASTM D573 and ISO 188 hold vulcanized rubber at a stated temperature and time, then remeasure hardness, tensile strength, and elongation at break against the unaged controls.
A small hardness rise with strong tensile and elongation retention means the network still looks like rubber. A large hardness jump with a sharp elongation drop means the compound is cooking: oxidation and further crosslinking harden the cord, cut flexibility, and open the door to heat cracking in service.
This article expands the heat-aging note in the O-Ring Temperature Guide into a full working explanation. It pairs with compression set testing (squeeze retention under heat) and TR-10 (cold recovery). Here the focus is oven aging effects on hardness, tensile, and elongation.
Temperature Guide Compression Set Failure Modes Ask About a Compound
Why heat aging matters for seals
An O-Ring seals because elastic contact stress presses rubber into the gland surfaces. Hot air changes that story even when no fluid is present:
- Hardness / modulus: oxidative aging usually stiffens the network. The cord gets harder and less forgiving of groove tolerances and thermal cycling.
- Tensile strength: retained strength shows whether the polymer still carries load after the soak. Large losses point to chain scission or severe network damage.
- Elongation at break: retained elongation is the flexibility story. A sharp drop means embrittlement risk on flex, install, or pressure pulse.
When heat aging climbs too far:
- Teardown shows a shiny, brittle ring that snaps instead of stretching.
- Surface cracks appear under strain (classic heat hardening and cracking).
- A ring that sealed at assembly weeps after a long hot dwell even when the groove never moved.
Heat aging is a temperature + time + air story. Pair it with compression set when the gland stays squeezed hot, and with fluid aging when chemistry rides along with the heat.
What heat aging is
Heat aging (also called air-oven aging, accelerated aging, or heat resistance) is the change in physical properties after vulcanized rubber sits in hot air under ASTM D573 (and the closely related ISO 188). Labs report property changes as absolute deltas (for example Shore A points) or as percent retention of the original tensile and elongation values.
In plain language: bake the rubber in a controlled oven, then ask how hard, strong, and stretchy it still is.
| Reading | What it means |
|---|---|
| Hardness rise | Network stiffened (typical oxidative crosslinking path) |
| Hardness drop | Softening / degradation path (less common in dry air; watch for that signal) |
| Tensile retention | Strength left after the soak (higher % is better) |
| Elongation retention | Stretch left after the soak (higher % is better; sharp loss tracks embrittlement) |
Two ideas get confused on datasheets:
| Term | What it answers |
|---|---|
| Heat aging (ASTM D573 / ISO 188) | How hardness, tensile, and elongation move after unconstrained (or loosely aged) hot-air exposure |
| Compression set (ASTM D395) | How much permanent thickness loss remains after a fixed squeeze, time, and temperature |
Heat aging ranks material damage in hot air. Compression set ranks squeeze recovery under deflection. Both belong on a hot-seal datasheet. A compound can look fine on free oven aging and still take a high set in a fixture, or the reverse.
Heat aging in one picture
Unaged rubber starts soft and stretchy. After oven aging, hardness usually rises and elongation falls. Report hours and °C beside every change number.
How the heat aging test works
ASTM D573 covers deterioration of vulcanized rubber in an air oven. ISO 188 is the common international counterpart and describes accelerated aging / heat-resistance methods in cell ovens and cabinet ovens with controlled air circulation. Seal-compound datasheets most often cite a stated °C and hours, then list hardness change plus tensile and elongation retention. Always read the temperature, time, and oven style on the report.
Heat aging test sequence
Typical ASTM D573 / ISO 188 air-oven workflow. Exact oven type, hours, and temperature belong on the datasheet line.
- 1 Measure unaged Record original hardness (Shore A or IRHD), tensile strength, and elongation at break on matched specimens (often ASTM D412 / ISO 37 dumbbells).
- 2 Load the oven Hang or place specimens so air can circulate. Keep different compounds separated when volatile cross-contamination is a risk.
- 3 Age Hold for the stated hours at the stated °C (commonly 70 h or 168 h; shorter 22–96 h screens also appear).
- 4 Cool & condition Remove specimens, cool, and condition at room temperature before retesting so readings are not still hot.
- 5 Report changes Δ hardness, % tensile retained, and % elongation retained. Report hours and temperature beside every number.
Specimen notes (typical practice)
- Die-cut tensile dumbbells from a cured slab are the usual laboratory path for tensile and elongation retention.
- Hardness buttons or slabs ride the same aging lot so ΔH matches the tensile set.
- Finished O-Ring sections can be aged when you want geometry closer to the seal. Thin cords often age faster than thick buttons because oxygen reaches more of the cross-section.
- Run multiple specimens per condition and average. One scorched outlier can move a borderline grade across a customer limit.
- Oven air changes per hour and cell vs cabinet construction matter for precision work. Compare like-with-like across candidate compounds.
- Fluid aging at temperature (immersion, then the same property checks) is a different, tougher ask than dry-air heat aging. Ask for it when the seal lives in hot oil, fuel, or process chemistry.
Match test temperature to the polymer and the duty
Compounds are usually screened near the heat capability of that polymer family, the same idea ASTM D2000 uses when it ties line-callouts to heat-aging temperatures. A nitrile datasheet often shows aging near 100 °C. An FKM grade is often screened near 200 °C or hotter. Those are fair comparisons inside each family. They are easy to misread across families or against a mild application.
Testing temperature by polymer (ASTM D2000)
Typical heat-aging screen temperatures tied to the ASTM D2000 classification letter. Exact datasheet hours still vary (22 h, 70 h, 168 h, and longer).
| Polymer | ASTM D2000 classification | Temperature |
|---|---|---|
| Natural rubber | AA | 70 °C |
| SBR | AA, BA | 70 °C, 100 °C |
| Butyl | AA, BA | 70 °C, 100 °C |
| EPDM | BA, CA, DA | 100 °C, 125 °C, 150 °C |
| Neoprene | BC, BE | 100 °C |
| Nitrile | BF, BG, BK, CH | 100 °C, 125 °C |
| Polyacrylate | DF, DH | 150 °C |
| Hypalon | CE | 125 °C |
| Urethane | BG | 100 °C |
| Silicone | GE | 200 °C |
| Fluorosilicone | FK | 200 °C |
| Fluorocarbon | HK | 250 °C |
Application trap: A large hardness rise measured at 150 °C does not automatically disqualify a compound for a near-room-temperature gland. Re-read the test temperature. If the duty is mild, ask for aging data closer to the real soak before you walk away from an otherwise good grade.
How seal engineers use heat aging in practice
Industry practice for O-Rings and similar compression seals:
Duty reading of heat aging
Hot static glands care about hardening and elongation loss. Dynamic glands add flex fatigue and wear on top of the same oven story.
Retain elongation · limit ΔH
Flanges, covers, and lids that sit hot for months need compounds that stay flexible enough to follow thermal cycles. Treat datasheet aging at or above your continuous soak as the first screen, then confirm compression set on the same temperature band.
Aging plus modulus and wear
Rods and shafts still embrittle from oven aging, and they also see friction heat, abrasion, and extrusion. Strong elongation retention with the wrong hardness or fluid swell is still a short seal life.
Modest ΔH · high %Eb
Small hardness rise and strong elongation retention after a fair screen mean the network still behaves like rubber at that temperature and time.
Hard + low stretch
Large Shore rise with a sharp elongation drop is field embrittlement waiting to happen. Teardown often matches heat hardening and cracking.
Dry air ≠ hot oil
Passing D573 in air does not prove fluid life. Add immersion aging or volume swell when chemistry is present.
Catalog check: Compare aging numbers only when hours and temperature match. A “+5 Shore / 80% elongation retained” at 70 °C for 70 h is not the same claim as the same numbers at 150 °C for 168 h.
Design takeaways
- Match the oven temperature to the continuous gland soak, with margin for hot spots.
- Read hardness change and elongation retention together. Hardness alone hides embrittlement.
- Pair heat aging with compression set for long-dwell squeeze. Free aging and fixture set answer different questions.
- After teardown, a brittle, cracked, shiny cord is field evidence of over-temperature or under-rated heat aging. See failure modes.
Typical heat capability by elastomer family
The chart below shows approximate continuous dry-heat midpoints used for family shortlisting (illustrative ranking, not a single ASTM D573 condition). Longer bars mean higher continuous heat capability. Real grades scatter with cure system, fillers, and stabilizers. Always use the grade datasheet aging line at your hours and °C.
Typical continuous dry-heat capability by family
Approximate commercial midpoints on a 70–300 °C scale. Color: green (higher heat) → teal → amber → red (lower heat). Rankings shift with intermittent spikes and fluid presence.
Width % ≈ (T − 70) ÷ 230 on a 70–300 °C scale. Use grade datasheet aging and set values at your hours and temperature for design.
| Family | Typical continuous dry heat | Aging notes for seals |
|---|---|---|
| FFKM | ~300 °C | Premium heat and chemical aging resistance; confirm grade and cost |
| FKM | ~200 °C | Strong hot-air and hot-oil aging; pair with fluid compatibility |
| Silicone (VMQ) | ~200 °C | Excellent dry-heat aging; watch tear, abrasion, and oil swell |
| Fluorosilicone | ~175 °C | Heat aging with better fuel/oil resistance than silicone |
| Aflas® (FEPM) | ~175–200 °C | Steam / amine heat path; confirm the exact aging condition |
| HNBR | ~135–150 °C | Clear step up from NBR on heat aging and strength |
| EPDM | ~135–150 °C | Strong water / steam / brake-fluid heat path in the right grades |
| NBR | ~100–120 °C | Everyday oil service; heat aging often sets the ceiling |
| Neoprene (CR) | ~100 °C | Outdoor / refrigerant heritage; confirm hot-air needs |
Shop starting points when dry heat and fluid both matter: Viton® / FKM, HNBR, EPDM, and Silicone.
Heat aging compared with compression set and TR-10
| Test | What it measures | When seal engineers reach for it |
|---|---|---|
| Heat aging (ASTM D573 / ISO 188) | Hardness / tensile / elongation shift after oven aging in air | Broader heat damage beyond set alone; compound heat ranking |
| Compression set (ASTM D395 / ISO 815) | Permanent thickness loss after fixed squeeze, time, and temperature | Primary long-dwell sealing-force screen |
| TR-10 (ASTM D1329 / ISO 2921) | Cold retraction temperature | Cold start floors after a heat-capable compound is chosen |
| Volume swell (ASTM D471 / ISO 1817) | Fluid-driven size and property change | Oil, fuel, and chemical service with heat |
| Hardness (Shore A / IRHD) | Indentation hardness before and after aging | Quantifies the stiffening or softening half of the oven story |
For hot O-Rings, use heat aging + compression set together. Aging tells you whether the rubber still looks like rubber. Set tells you whether it still pushes back in the groove. Add TR-10 when the same gland also sees cold starts.
Reading a datasheet without getting fooled
- Find heat aging (or air oven / ASTM D573 / ISO 188), then read hours and temperature.
- Read hardness change beside tensile and elongation retention. A modest ΔH with a collapsed elongation is still an embrittlement risk.
- Confirm whether the specimen was dry-heat or fluid-aged.
- Compare only like-with-like across candidate grades.
- Check compression set on a matching temperature band for long-dwell glands.
- Ask whether the marketed “continuous temperature” equals a real aging screen or a short peak rating.
Application trap: A strong 70-hour air-oven result does not prove 5,000 hours in hot oil. Re-match fluid and dwell. Use the Temperature Guide with grade aging data, and immerse when chemistry is part of the duty.
Practical selection checklist
- Write down max continuous soak temperature, peak spikes, dwell time, and static vs dynamic duty.
- Shortlist families that cover the heat end on the Temperature Guide, then confirm fluid compatibility.
- Compare heat aging on matching hours / °C: hardness change plus tensile and elongation retention.
- Check compression set at a temperature near the soak.
- For cold starts, add TR-10.
- Validate critical glands with the real compound, squeeze, and environment. Datasheet oven aging is a screen, not a full life proof.
Quick answers
What does heat aging mean?
It is the change in rubber properties after a stated time in a hot-air oven under ASTM D573
/ ISO 188. Seal datasheets usually report hardness change and percent retention of
tensile strength and elongation at break. Report hours and temperature beside every number.
Is a +8 Shore hardness rise after aging acceptable?
It depends on the test condition and the duty. Eight points after 70 h at 100 °C can be
routine for some nitrile grades. Eight points after 70 h at 200 °C on an FKM screen is a
different conversation. Always read elongation retention beside the hardness delta.
Why did my O-Ring come out hard and cracked?
Long dwell above the compound’s continuous rating, hot spots, or oxidative aging are the
usual causes. See
heat hardening and cracking.
How is heat aging different from compression set?
Heat aging tracks free (or loosely aged) property damage in hot air. Compression set tracks
permanent thickness loss after a fixed squeeze. Hot static lids need both: aging for
embrittlement risk, set for lost sealing force.
Does passing D573 prove cold sealing?
No. Oven aging is a heat story. For cold starts, use
TR-10 and the
Temperature Guide.
Where should I go next?
Start with the Temperature Guide, then
compression set and
TR-10. Material pages for
Nitrile,
HNBR,
EPDM,
FKM / Viton®, and
Silicone
carry family heat ranges.
Contact The O-Ring Store with fluid, pressure, static vs dynamic
duty, and the hottest continuous temperature you must survive.
Heat aging values vary by compound, cure, oven style, and test condition. Use grade-specific data for design decisions, and validate critical seals under the real temperature and dwell profile.
